Friday, February 2, 2018

7mm-08 Project #18

Timing Action Screws

I like to make sure that all of my screw heads run "north and south". Meaning that they are aligned running parallel with the barrel. I think that it is a nice touch on a custom rifle. 

This rifle was pillar bedded, meaning that there are aluminum pillars bonded in where the action screw go through the stock. This makes it really easy to have repeatable bedding using a torque wrench to tighten the action screws. It also means that the screws will return to the same place every time. 
 First I assemble the rifle and tighten the screws to the necessary torque. Then I take note of how far the screw head needs to rotate (Angle in degrees). Then I install a dial indicator and turn the screw the same amount in the oppisite direction (see the tape marks) and measure how far it moves. At this point I know how much material I need to remove to make the screw turn the correct angle to line up. Who says that math is useless! 
 Then the screw is taken to the lathe and the computed amount is removed from the underside of the screw. The screw is then deburred and polished. 
If done correctly you will end up with your screws lined up "north and south" 

Thursday, February 1, 2018

7mm-08 Project #17

Sling Swivels

In this post I will cover how I inlet Sling Swivels. 
 First, I make the brass threaded inserts that I will bond into the stock (I have covered it many times in other posts so I will not repeat it here) then I file down the screw heads and align them so that the screws are running "north and south".
 I mount the stock in a fixture that I built to hold the stock in place so that I can cut the recesses on the mill. Shims and Clamps are used to get it aligned and clamped in place. If something slipped at this point and damaged the stock I am not sure what I would do!
 Here is the mill cutter cutting the slot. 
A clean slot that has just been machined. 
 A test fit and it looks perfect. 

 Then on to the front slot. 
 Again a perfect fit. 

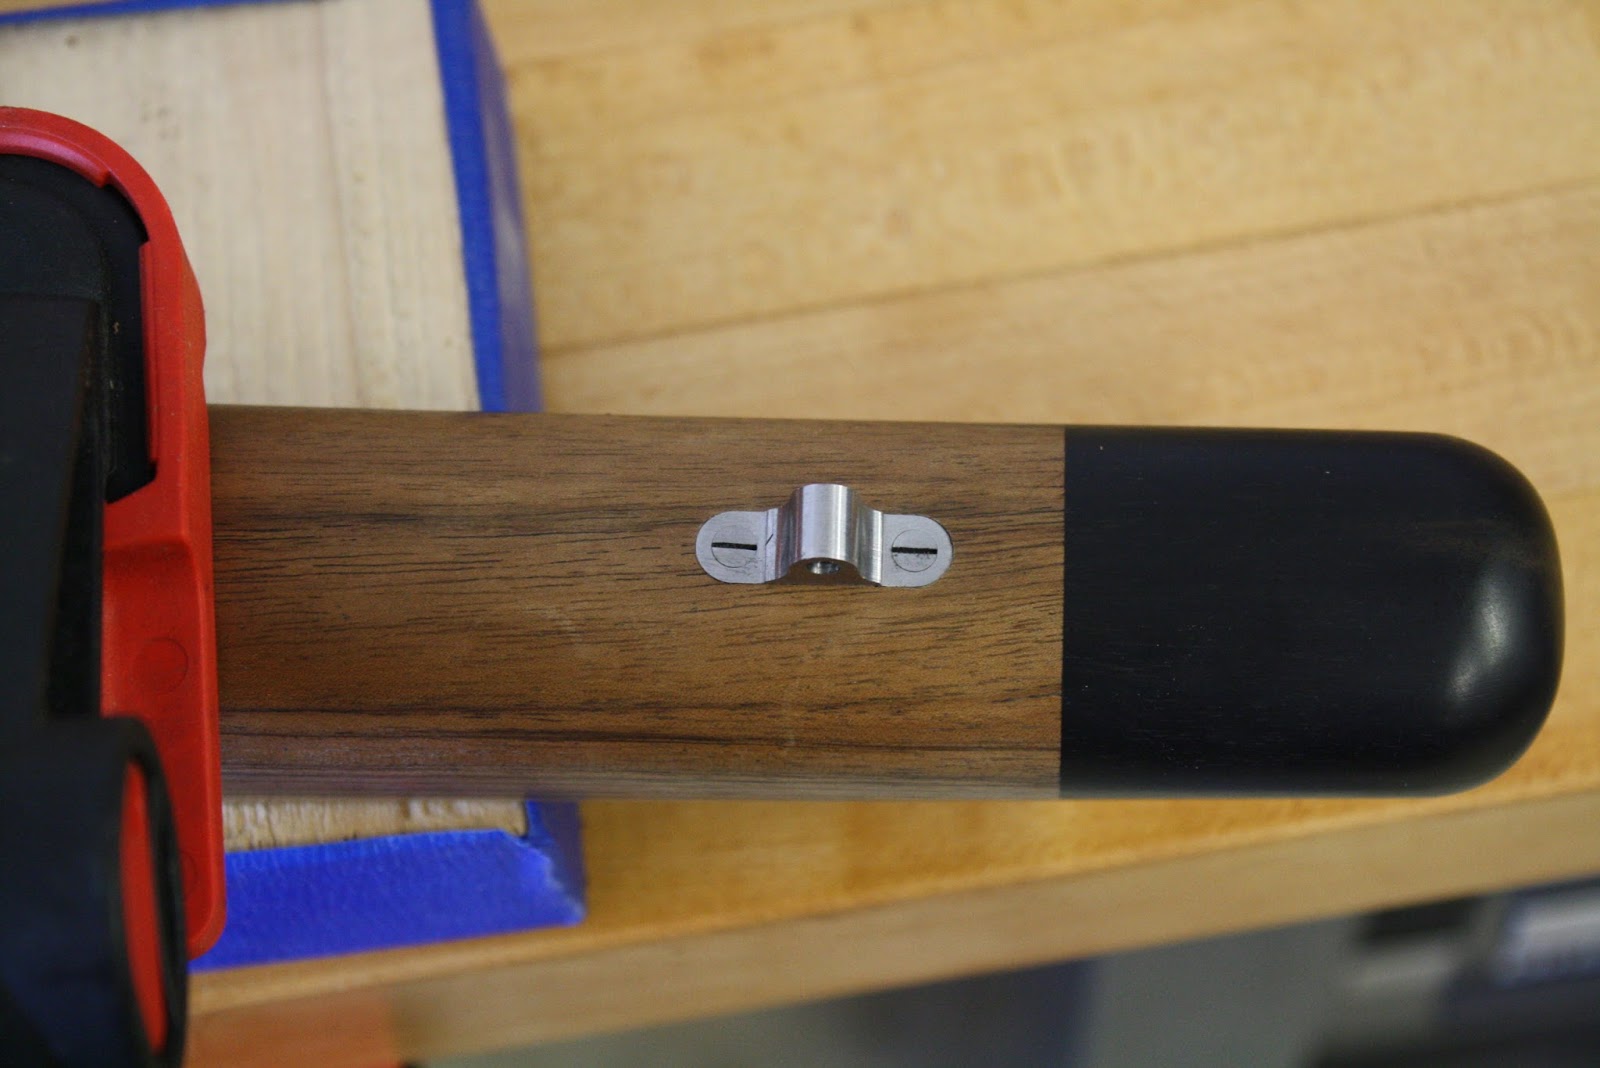
 The swivel then has the brass inserts screwed back on and the brass is bonded to the stock. After a little filing and sanding they look like this. Job done! 

Some consider this cheating because I am using machine tools instead of scrapers and chisels. I think of myself as a Gunbuilder (Hack Gunbuilder actually) not an artist. So I am completely fine using modern tools. I don't believe that it is better just because it is harder. But that is just my opinion.

I will admit that if I walked into Holland and Holland in London and they had automted everything I would be a little disappointed.   

Wednesday, January 31, 2018

7mm-08 Project #16

Stock Shaping 

I am going to show you a few examples of the detail cleanup work that is done on the stock. I don't have pictures of all the work that was done but this is an example of the cleanup in two areas.
Initial sanding and shaping of the stock has started. Most of the rough machine marks on the outside of the stock have been filed off and sanded smooth. Now I start the detail work. 
 Here is the ejection cutout after inletting. It is a nice clean fit but I like to dress this area up a little. 
 
 I first start by extending the radius on the sides further down the stock. I call this cutting in the fangs. 
 Then I file the area between them flat, this is a picture part way through the process. 
Here is the completed cutout ready for final sanding. I think that this adds a nice touch. You can also see that the ebony cross bolts have been sanded down and cleaned up. 
 Then I turn my attention to other areas of the stock that need to be cleaned up. Here the top of the grip is getting cleaned up. This is the grip in the rough form. 
 Here I have started to contour the grip to a more pleasing contour. 
Here is the grip finished ready for final sanding. 

This process is completed in several other places of the stock but I don't have pictures of all of them. 

Monday, January 29, 2018

7mm-08 Project #15

Finishing up the Recoil Pad

In this post I will complete the recoil pad installation. 
First the recoil pad is mounted on the stock and a line is scribed around the edge of the pad where the stock meets. This will be a reference during the sanding down of the pad.
 I like to use a recoil pad fixture. This allows me to mount pads on stocks that are finished without marring the finish (not an issue with this stock but it is my preferred method). Here I am setting the stop on the fixture so that after I grind the toe of the pad I can return the fixture to 90 degrees to grind the other sides. 
 Then I set the angle of the toe of the pad. I will start grinding with the toe and then return the fixture to the stop I set in the previous step for the sides and the top. 

 The pad is mounted in the fixture upside down and the scribe line is filled with chalk dust to that it can be seen easily. Here I am grinding the toe angle. 
 Once the toe is complete I return the fixture to the stop I set and grind the sides and top. You can see that the layout line is still visible on the sides and top but not the toe area that has been completed. 
Here is the finished pad mounted to the stock. It is starting to look like a Rifle! 

Sunday, January 28, 2018

7mm-08 Project #14

Recoil Pad 2

Installation of the recoil pad continued.
 The center line of the stock is marked and one of the hole locations is marked and center punched for drilling. 
 Here the top hole is drilled. From here a jig will be used to identify the location of the bottom hole and hold everything during the gluing operation. 
 The second hole has been marked and drilled and everything is fit checked prior to gluing. The aluminum piece is a jig that I made to hold everything in place. The jig has the same hole spacing as the recoil pad. This will insure that everything lines up after bonding. Sorry about the blurry picture. 
 Epoxy has been applied and the jig assembly is taped down to hold everything in place while the glue cures. 
Here is a shot of the brass spacers bonded in ready to accept the recoil pad. Finish has been applied to seal the end grain. 

Saturday, January 27, 2018

7mm-08 Project #13

Recoil Pad 

Just like the grip cap I like to use brass inserts when installing recoil pads. This does several things but most importantly in insures that the pad always lines up in the same place after installation and removal. It also creates a much stronger mount than putting wood screws into the end grain. Plus I think that it is a nice touch and worth the effort.
 Here is a brass machine screw getting the head cut off in the lathe
 Drilling a hole to accept threads for the mounting screws. 
 Tapping the hole to accept the mounting screw.
 Here are all the components ready to mount on the stock. I have the wood screws that came with the pad shown for reference (they will not be used). I have also included the screwdriver bit that I use to install pads. This is a standard Phillips bit, but I have polished the outside so that it does not mar the recoil pad holes when tightening the screws. It is important to lubricate this bit with, soap, water, or wax when installing the pad so the screw holes don't get marred. 
 Here I am laying out the cut line for the stock. At this point you can adjust the angle of the pad. I usually make mine 90 degrees to the bore line.
Here is the stock cut down ready to start installing the pad. Cutting the stock always makes me nervous! 

Friday, January 26, 2018

7mm-08 Project #12

Grip Cap Cont.

After installing the grip cap the profile of the grip needs to be shaped. As you can see the semi-inletted blank has a lot more material in the grip area than we need. It will have to be filled down to match the profile. 
 First the front is filed almost down to the grip cap.
 Then each side is filed down starting 45 degrees from the front. The line of the filing is carried all the way up the grip.
 Then two more flats are added, and carried up the grip.
 This is done until you have many flats filed up to the cap. This looks like a radius but it is actually many flat facets. If you look close you can see them. 
Then you smooth out the areas between the flats and you end up with a curve that matches the grip cap. The wood is left a little proud of the cap at this point. It will be brought down to the cap during the stock sanding. 

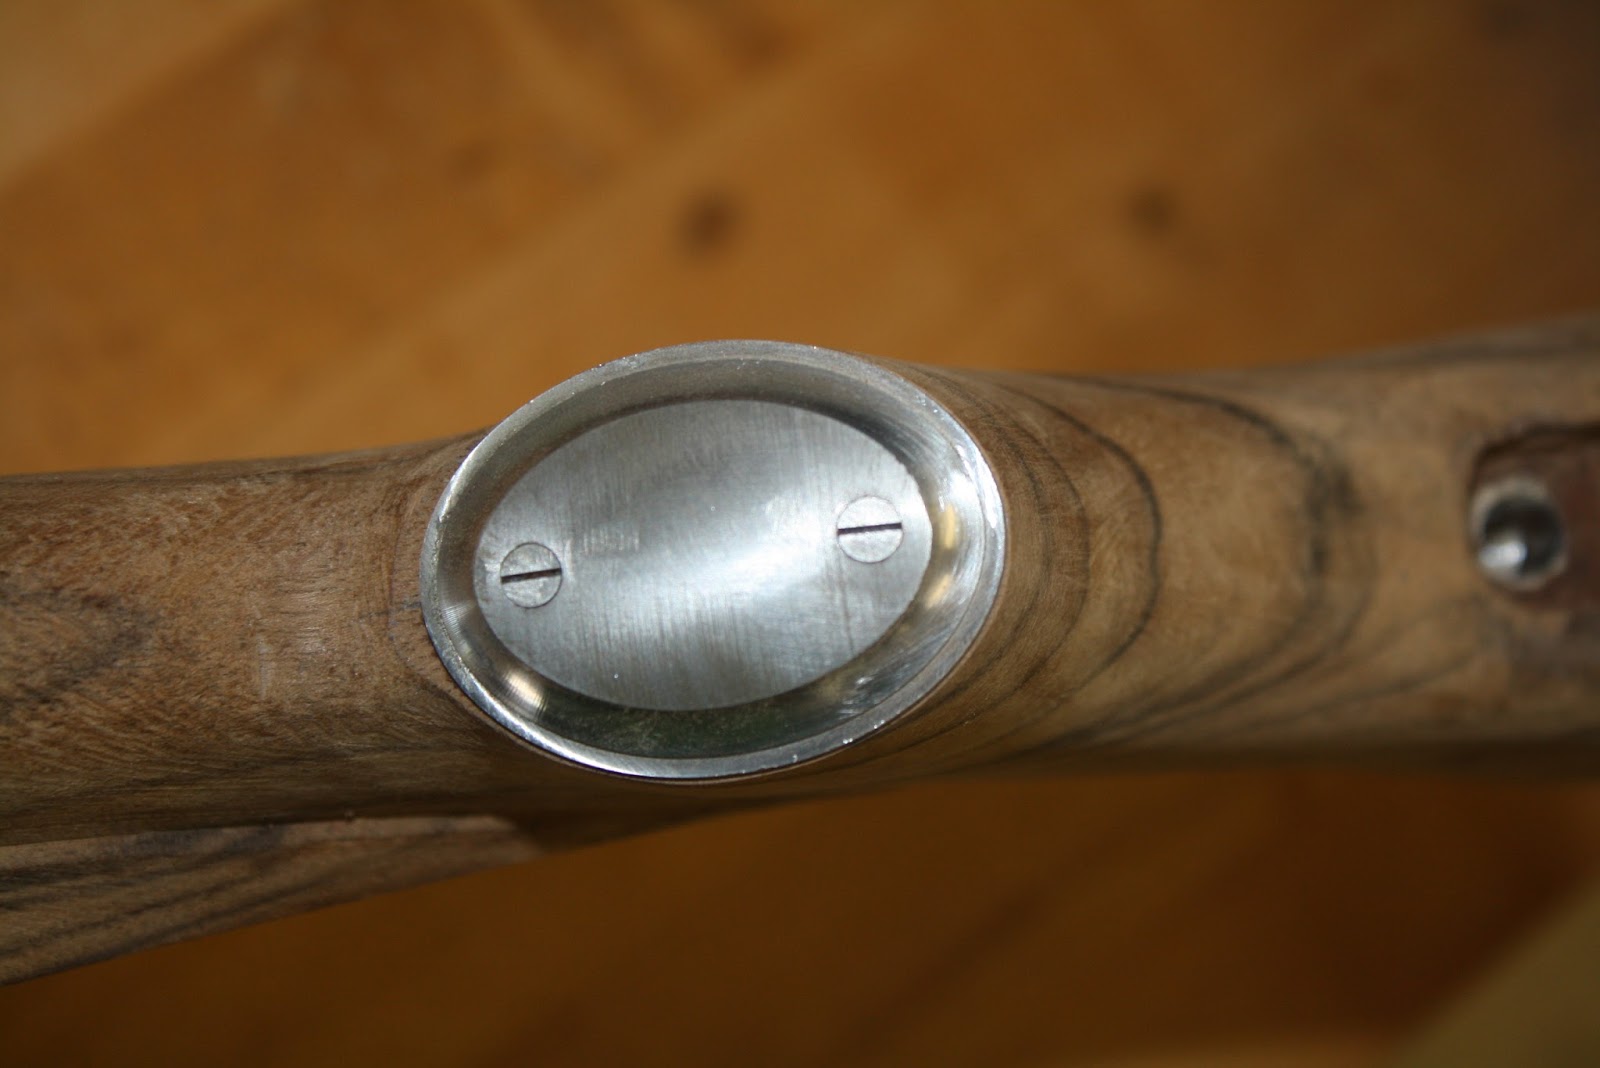
You can see that the screw heads have also been dressed down to the cap. The cap and screw heads will be polished later.